GX4CrNiMo16-5-1 (EN 1.4405) Martensitic Stainless Steel Casting Material
Martensitic Stainless Steel
Introduction
GX4CrNiMo16-5-1 is a martensitic stainless steel grade specified in EN 10283 for corrosion-resistant cast components. Casting process options include Investment Casting, Shell Molding Casting and Sand Casting, subject to the applicable specification and component requirements.
| Field | Value |
|---|---|
| Designation | GX4CrNiMo16-5-1 (EN 1.4405) |
| Material Type | Stainless Steel |
| Sub Type | Martensitic Stainless Steel |
| Product Form | casting |
Manufacturing Process
Investment Casting
Shell Molding Casting
Sand Casting
Equivalent Grades
N/A
Similar Materials
N/A
Reference Standards
| Standard | Standard Title | Edition | Specification | Identifier |
|---|---|---|---|---|
| EN 10213 | Steel castings for pressure purposes | 2007+A1:2016 | GX4CrNiMo16-5-1 | EN 1.4405 |
| EN 10283 | Corrosion resistant steel castings | 2019 | GX4CrNiMo16-5-1 | EN 1.4405 |
| EN 10293 | Steel castings — Steel castings for general engineering uses | 2015 | GX4CrNiMo16-5-1 | EN 1.4405 |
| EN 10340 | Steel castings for structural uses | 2007 | GX4CrNiMo16-5-1 | EN 1.4405 |
| ISO 11972 | Corrosion-resistant cast steels for general applications | 2023 | GX4CrNiMo16-5-1 | EN 1.4405 |
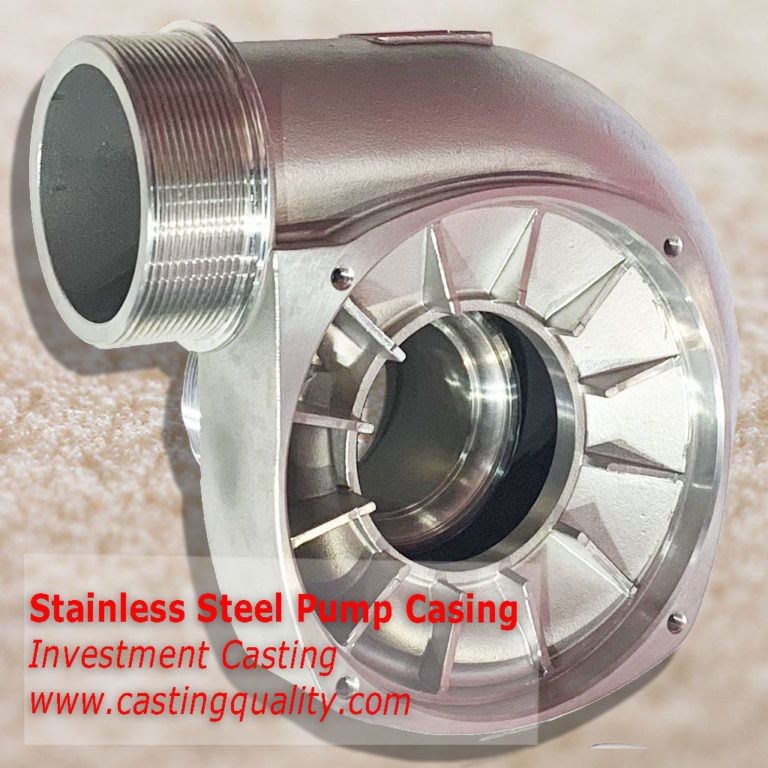
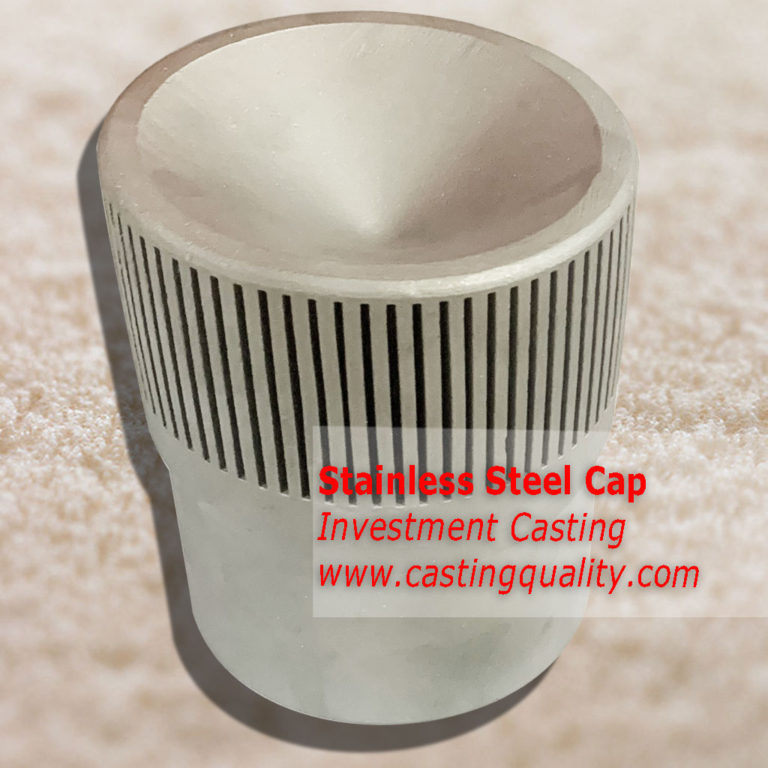
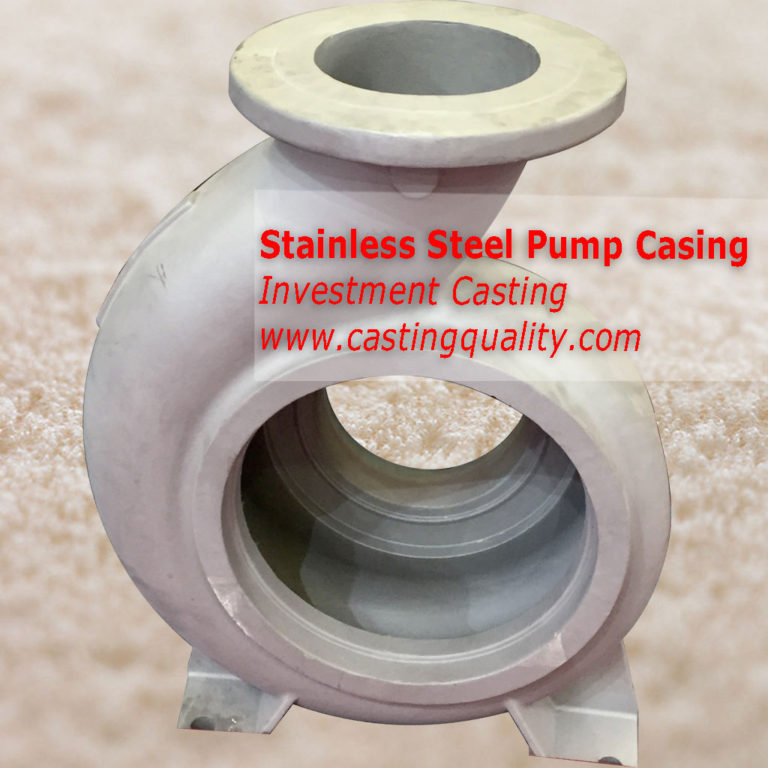
Related Casting Products
Physical Properties
EN 10213–2007+A1:2016
| Property | Value | Note |
|---|---|---|
| Density | 7.8 kg/dm³ | Test at 20 °C |
| Thermal Expansion | 10.8 ×10⁻⁶/K | Temperature range: 20–100 °C |
| Thermal Expansion | 11.5 ×10⁻⁶/K | Temperature range: 20–300 °C |
| Thermal Expansion | 12 ×10⁻⁶/K | Temperature range: 20–500 °C |
| Thermal Conductivity | 17 W/(m·K) | Test at 50 °C |
| Thermal Conductivity | 18 W/(m·K) | Test at 100 °C |
| Specific Heat | 460 J/(kg·K) | Test at 20 °C |
| Magnetic Property | Magnetic |
EN 10283–2019
| Property | Value | Note |
|---|---|---|
| Density | 7.8 kg/dm³ | Test at 20 °C |
| Specific Heat | 460 J/(kg·K) | Test at 20 °C |
| Thermal Conductivity | 17 W/(m·K) | Test at 50 °C |
| Thermal Conductivity | 18 W/(m·K) | Test at 100 °C |
| Thermal Expansion | 10.8 ×10⁻⁶/K | Temperature range: 20–100 °C |
| Thermal Expansion | 11.5 ×10⁻⁶/K | Temperature range: 20–300 °C |
| Thermal Expansion | 12 ×10⁻⁶/K | Temperature range: 20–500 °C |
Chemical Composition
| Element | EN 10213Edition 2007+A1:2016 · wt.%Cast analysis | EN 10283Edition 2019 · wt.%Cast analysis | EN 10293Edition 2015 · wt.%Cast analysis | EN 10340Edition 2007 · wt.%Cast analysis |
|---|---|---|---|---|
| C | ≤ 0.06 | ≤ 0.06 | ≤ 0.06 | ≤ 0.06 |
| Si | ≤ 0.80 | ≤ 0.80 | ≤ 0.80 | ≤ 0.80 |
| Mn | ≤ 1.00 | ≤ 1.00 | ≤ 1.00 | ≤ 1.00 |
| P | ≤ 0.035 | ≤ 0.035 | ≤ 0.035 | ≤ 0.035 |
| S | ≤ 0.025 | ≤ 0.025 | ≤ 0.025 | ≤ 0.025 |
| Cr | 15.00–17.00 | 15.00–17.00 | 15.00–17.00 | 15.00–17.00 |
| Ni | 4.00–6.00 | 4.00–6.00 | 4.00–6.00 | 4.00–6.00 |
| Mo | 0.70–1.50 | 0.70–1.50 | 0.70–1.50 | 0.70–1.50 |
| Cu | ≤ 0.30 | ≤ 0.30[1] | ≤ 0.30[2] | ≤ 0.30 |
| N | — / Not specified | — / Not specified | — / Not specified | ≤ 0.08 |
| V | ≤ 0.08 | ≤ 0.08[1] | ≤ 0.08[2] | — / Not specified |
Notes
EN 10283 · Edition 2019
[1] Cu/V: Applies unless otherwise agreed; unspecified elements shall not be intentionally added without purchaser agreement except for finishing the heat.
EN 10293 · Edition 2015
[2] Cu/V: Applies only where unspecified in unless otherwise agreed; no intentional addition except for finishing the heat.
Heat Treatment
EN 10213–2007+A1:2016 · +QT
EN 10283–2019 · +QT
| Step | Operation | Temperature | Cooling |
|---|---|---|---|
| 1 | quenching | 1020–1070 °C | air or liquid |
| 2 | tempering | 580–630 °C | — |
EN 10293–2015 · +QT
| Step | Operation | Temperature | Cooling |
|---|---|---|---|
| 1 | : quenching | 1020–1070 °C | air |
| 2 | : tempering | 580–630 °C | — |
EN 10340–2007 · +QT
| Step | Operation | Temperature |
|---|---|---|
| 1 | : quenching | 1020–1070 °C |
| 2 | : tempering | 580–630 °C |
ISO 11972–2023 · Heat treated
| Step | Operation | Temperature | Cooling |
|---|---|---|---|
| 1 | austenitizing | 1020–1070 °C | air cool |
| 2 | tempering | 580–630 °C | air or furnace cool |
Notes
EN 10213 · Edition 2007+A1:2016
[1] +QT: Treatment temperatures are given for information; required delivery condition is specified separately.
Mechanical Properties
| Property | EN 10213Edition 2007+A1:2016 | EN 10283Edition 2019[1] | EN 10293Edition 2015[2] | EN 10340Edition 2007[3] | ISO 11972Edition 2023[4] |
|---|---|---|---|---|---|
| Yield Strength (Rp0.2) | ≥ 540 MPa[5] ≥ 515 MPa[6] ≥ 485 MPa[7] ≥ 455 MPa[8] | ≥ 540 MPa | ≥ 540 MPa | ≥ 540 MPa | ≥ 540 MPa |
| Tensile Strength | 760–960 MPa[5] | ≥ 760 MPa | 760–960 MPa | 740–960 MPa | ≥ 760 MPa |
| Elongation | ≥ 15 %[5] | ≥ 15 % | ≥ 15 % | ≥ 15 % | ≥ 15 % |
| Impact Energy | ≥ 60 J[5] | ≥ 60 J[9] | ≥ 60 J | ≥ 60 J | ≥ 60 J[10] |
Notes
EN 10283 · Edition 2019
[1] All properties in this column: wall thickness ≤ 300 mm; Test block; maximum thickness 150 mm; Room temperature; Yield and tensile strength also apply to the casting up to the maximum specified wall thickness.
[9] Impact Energy: KV2 as specified in
EN 10293 · Edition 2015
[2] All properties in this column: wall thickness ≤ 300 mm; Test block of relevant thickness; maximum test-block wall thickness 150 mm; Room temperature; Properties apply to the casting up to the specified maximum wall thickness; above this, foreseeable lowering shall be agreed.
EN 10340 · Edition 2007
[3] All properties in this column: wall thickness ≤ 300 mm; Test block of relevant thickness; maximum thickness 150 mm; Room temperature; Yield and tensile strength also apply to the casting up to the maximum relevant wall thickness.
ISO 11972 · Edition 2023
[4] All properties in this column: wall thickness ≤ 300 mm; Room temperature; Test blocks used to verify mechanical properties shall not exceed 150 mm thickness. Properties for samples removed from castings shall be agreed between manufacturer and purchaser.
[10] Impact Energy: Verification of impact tests is required only when indicated by the customer.
EN 10213 · Edition 2007+A1:2016
[5] Yield Strength (Rp0.2)/Tensile Strength/Elongation/Impact Energy: wall thickness ≤ 300 mm; Properties verified on test blocks of thickness up to 150 mm; applicability to casting wall thickness as stated. Larger governing thickness requires agreement.; Room temperature
[6] Yield Strength (Rp0.2): Test at 100 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[7] Yield Strength (Rp0.2): Test at 200 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[8] Yield Strength (Rp0.2): Test at 300 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
Welding Conditions
EN 10213–2007+A1:2016
EN 10283–2019
EN 10293–2015
| Requirement | Value |
|---|---|
| Preheat | No preheat[7] |
| Interpass Temperature | ≤ 200 °C |
| Post-weld Heat Treatment | Same as base-material tempering temperature |
EN 10340–2007
| Requirement | Value |
|---|---|
| Preheat | No preheat[8] |
| Interpass Temperature | ≤ 200 °C |
| Post-weld Heat Treatment | Same as the base-material tempering temperature |
Notes
EN 10213 · Edition 2007+A1:2016
[1] Preheat: Production welding by the foundry; ferritic/martensitic guidance is informative.; Preheat temperature depends on casting geometry, thickness and climatic conditions.
[2] Interpass Temperature: Production welding by the foundry; ferritic/martensitic guidance is informative.
[3] Post-weld Heat Treatment: Production welding by the foundry; ferritic/martensitic guidance is informative.; In general, production welds are major when prepared cavity depth exceeds 40% of the wall thickness; minor weld corrosion conditions may require special agreement.
EN 10283 · Edition 2019
[4] Preheat: Preheat depends on casting geometry, thickness and climatic conditions.
[5] Post-weld Heat Treatment: minor welds
[6] Post-weld Heat Treatment: major welds
EN 10293 · Edition 2015
[7] Preheat: Preheat depends on casting geometry, thickness and climatic conditions.
EN 10340 · Edition 2007
[8] Preheat: Preheat depends on casting geometry, thickness and climatic conditions.
Applications
Typical casting applications include valve and pump castings and general engineering components.
Last Updated: October 16, 2026