GX2CrNiMo19-11-2 (EN 1.4409) Austenitic Stainless Steel Casting Material
Austenitic Stainless Steel
Introduction
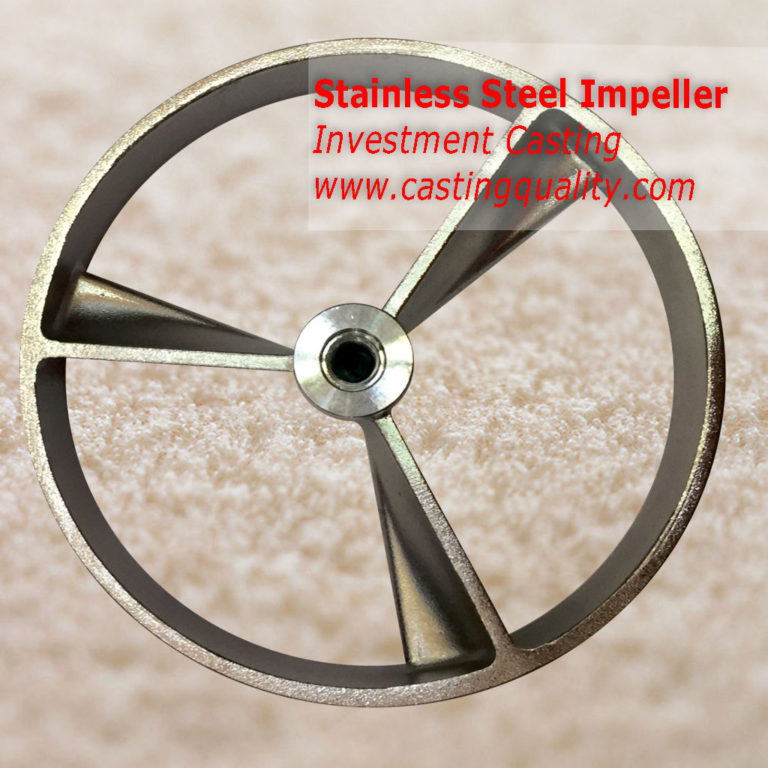
GX2CrNiMo19-11-2 is an austenitic stainless steel grade covered by EN 10213, EN 10283, EN 10340, ISO 11972. Typical family applications include pump casings, impellers, valve bodies, covers and pipe fittings.
| Field | Value |
|---|---|
| Designation | GX2CrNiMo19-11-2 (EN 1.4409) |
| Material Type | Stainless Steel |
| Sub Type | Austenitic Stainless Steel |
| Product Form | casting |
Manufacturing Process
Investment Casting
Shell Molding Casting
Sand Casting
Equivalent Materials
Similar Materials
N/A
Reference Standards
| Standard | Standard Title | Edition | Specification | Identifier |
|---|---|---|---|---|
| EN 10213 | Steel castings for pressure purposes | 2007+A1:2016 | GX2CrNiMo19-11-2 | EN 1.4409 |
| EN 10283 | Corrosion resistant steel castings | 2019 | GX2CrNiMo19-11-2 | EN 1.4409 |
| EN 10340 | Steel castings for structural uses | 2007 | GX2CrNiMo19-11-2 | EN 1.4409 |
| ISO 11972 | Corrosion-resistant cast steels for general applications | 2023 | GX2CrNiMo19-11-2 | EN 1.4409 |
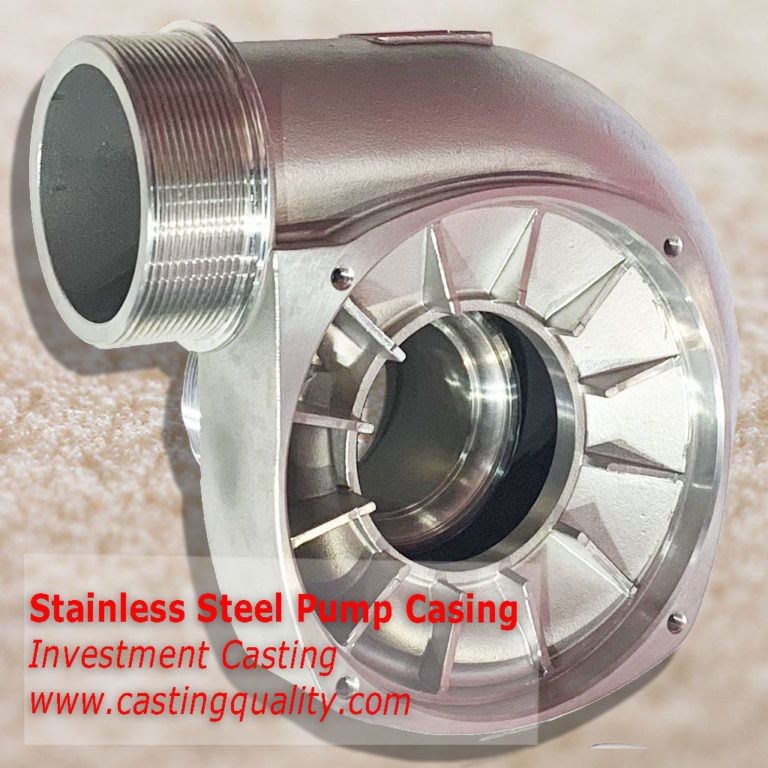
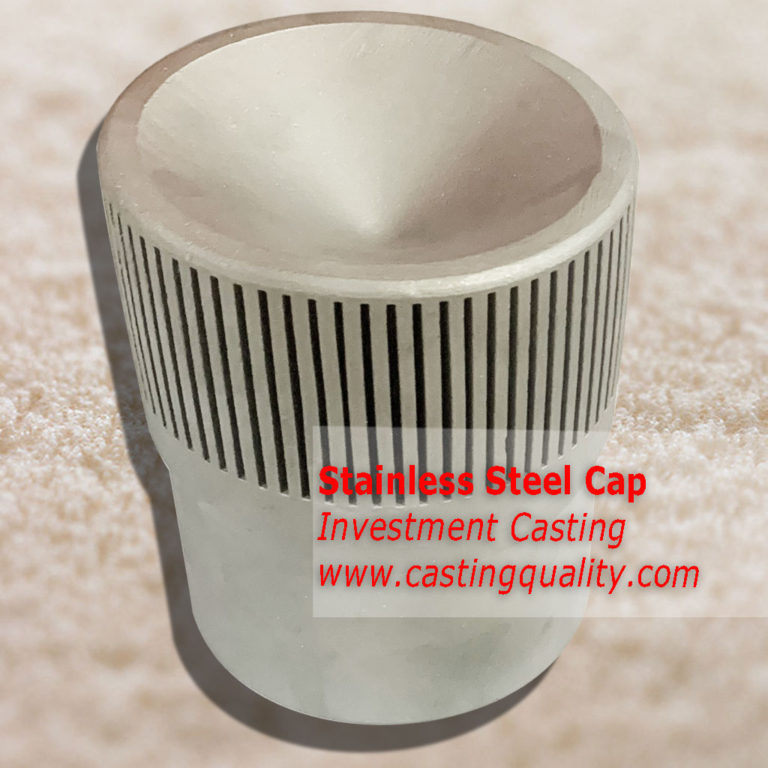
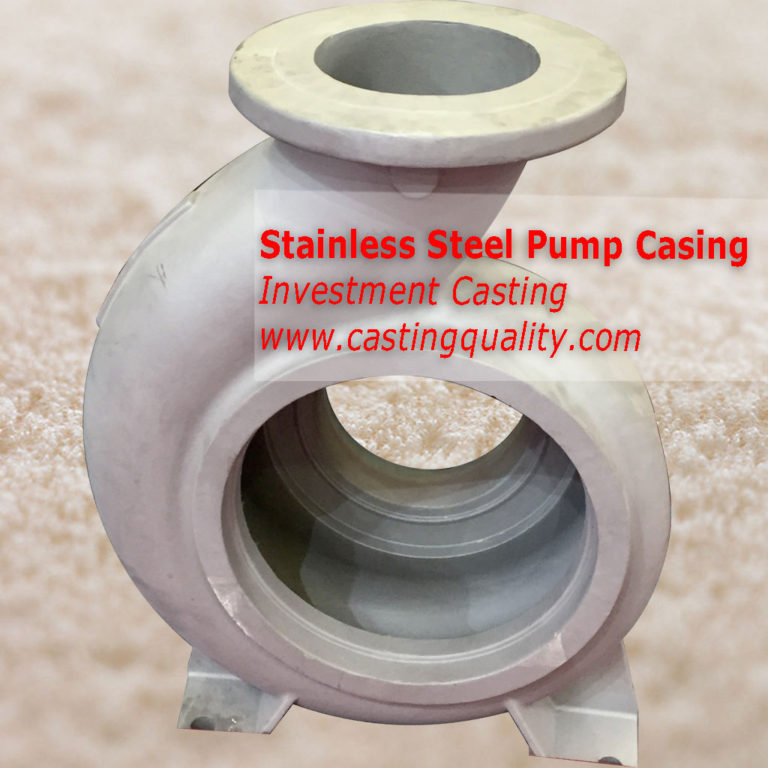
Related Casting Products
Physical Properties
| Property | Value / Unit | Note | Source |
|---|---|---|---|
| Density | 7.9 kg/dm³ | Test at 20 °C | EN 10213; EN 10283 |
| Thermal Expansion | 15.8 ×10⁻⁶/K | Temperature range: 20–100 °C | EN 10213 |
| Thermal Expansion | 17 ×10⁻⁶/K | Temperature range: 20–300 °C | EN 10213 |
| Thermal Expansion | 17.7 ×10⁻⁶/K | Temperature range: 20–500 °C | EN 10213 |
| Thermal Conductivity | 14.5 W/(m·K) | Test at 50 °C | EN 10213 |
| Thermal Conductivity | 15.8 W/(m·K) | Test at 100 °C | EN 10213 |
| Specific Heat | 530 J/(kg·K) | Test at 20 °C | EN 10213 |
| Magnetic Property | Not or slightly magnetic | EN 10213 | |
| Specific Heat | 530 J/(kg·K) | Test at 20 °C | EN 10283 |
| Thermal Conductivity | 14.5 W/(m·K) | Test at 50 °C | EN 10283 |
| Thermal Conductivity | 15.8 W/(m·K) | Test at 100 °C | EN 10283 |
| Thermal Expansion | 15.8 ×10⁻⁶/K | Temperature range: 20–100 °C | EN 10283 |
| Thermal Expansion | 17 ×10⁻⁶/K | Temperature range: 20–300 °C | EN 10283 |
| Thermal Expansion | 17.7 ×10⁻⁶/K | Temperature range: 20–500 °C | EN 10283 |
Chemical Composition
| Element | EN 10213Edition 2007+A1:2016 · wt.%Cast analysis | EN 10283Edition 2019 · wt.%Cast analysis | EN 10340Edition 2007 · wt.%Cast analysis | ISO 11972Edition 2023 · wt.% |
|---|---|---|---|---|
| C | ≤ 0.030 | ≤ 0.030 | ≤ 0.030 | ≤ 0.03 |
| Si | ≤ 1.50 | ≤ 1.50 | ≤ 1.50 | ≤ 1.5 |
| Mn | ≤ 2.00 | ≤ 2.00 | ≤ 2.00 | ≤ 2.0 |
| P | ≤ 0.035 | ≤ 0.035 | ≤ 0.035 | ≤ 0.035 |
| S | ≤ 0.025 | ≤ 0.025 | ≤ 0.025 | ≤ 0.025 |
| Cr | 18.00–20.00 | 18.00–20.00 | 18.00–20.00 | 18.0–20.0 |
| Ni | 9.00–12.00 | 9.00–12.00 | 9.00–12.00 | 9.0–12.0 |
| Mo | 2.00–2.50 | 2.00–2.50 | 2.00–2.50 | 2.00–2.50 |
| Cu | ≤ 0.50 | ≤ 0.50[1] | ≤ 0.50 | — / Not specified |
| N | ≤ 0.20 | ≤ 0.20 | ≤ 0.20 | ≤ 0.20 |
Notes
EN 10283 · Edition 2019
[1] Cu: Applies unless otherwise agreed; unspecified elements shall not be intentionally added without purchaser agreement except for finishing the heat.
Heat Treatment
EN 10213–2007+A1:2016 · +AT
| Step | Operation | Temperature | Cooling |
|---|---|---|---|
| 1 | Informative: solution annealing | 1080–1150 °C[1] | water quench |
EN 10283–2019 · +AT
| Step | Operation | Temperature | Cooling |
|---|---|---|---|
| 1 | solution annealing | 1080–1150 °C | water |
EN 10340–2007 · +AT
| Step | Operation | Temperature | Cooling |
|---|---|---|---|
| 1 | Informative: solution annealing | 1080–1150 °C | water |
ISO 11972–2023 · Solution treated
| Step | Operation | Temperature | Cooling |
|---|---|---|---|
| 1 | solution treatment | 1080–1150 °C[2] | quench |
Notes
EN 10213 · Edition 2007+A1:2016
[1] +AT: Treatment temperatures are given for information; required delivery condition is specified separately.
ISO 11972 · Edition 2023
[2] Solution treated: Depending on thickness, accelerated air cooling.
Mechanical Properties
Core Mechanical Properties
EN 10213 — 2007+A1:2016 · Table 3 — Normative
EN 10283 — 2019 · Table 2 — Normative
| Property | +AT |
|---|---|
| Yield Strength (Rp0.2) | ≥ 195 MPa |
| Yield Strength (Rp1.0) | ≥ 220 MPa |
| Tensile Strength | ≥ 440 MPa |
| Elongation | ≥ 30 % |
| Impact Energy | ≥ 80 J[2] |
- wall thickness ≤ 150 mm; Test block; maximum thickness 150 mm; Room temperature; Yield and tensile strength also apply to the casting up to the maximum specified wall thickness.
EN 10340 — 2007 · Table 2 — Normative
| Property | +AT |
|---|---|
| Yield Strength (Rp0.2) | ≥ 195 MPa |
| Tensile Strength | 440–640 MPa |
| Elongation | ≥ 30 % |
| Impact Energy | ≥ 80 J |
- wall thickness ≤ 150 mm; Test block of relevant thickness; maximum thickness 150 mm; Room temperature; Yield and tensile strength also apply to the casting up to the maximum relevant wall thickness.
ISO 11972 — 2023 · Table 2 — Normative
| Property | Solution treated |
|---|---|
| Yield Strength (Rp0.2) | ≥ 195 MPa |
| Tensile Strength | ≥ 440 MPa |
| Elongation | ≥ 30 % |
| Impact Energy | ≥ 80 J[3] |
| Yield Strength (Rp1.0) | ≥ 220 MPa |
- wall thickness ≤ 150 mm; Room temperature; Test blocks used to verify mechanical properties shall not exceed 150 mm thickness. Properties for samples removed from castings shall be agreed between manufacturer and purchaser.
Additional Mechanical Properties
Elevated-Temperature Properties
Low-Temperature Properties
EN 10213 — 2007+A1:2016 · Table 5 — Normative
| Property | +AT |
|---|---|
| Impact Energy | ≥ 70 J[8] |
Notes
EN 10213 · Edition 2007+A1:2016
[1] Yield Strength (Rp1.0)/Tensile Strength/Elongation/Impact Energy: wall thickness ≤ 150 mm; Properties verified on test blocks of thickness up to 150 mm; applicability to casting wall thickness as stated. Larger governing thickness requires agreement.; Room temperature
[4] Yield Strength (Rp1.0): Test at 100 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[5] Yield Strength (Rp1.0): Test at 200 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[6] Yield Strength (Rp1.0): Test at 300 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[7] Yield Strength (Rp1.0): Test at 400 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[8] Impact Energy: Test at -196 °C; Test block; maximum thickness 150 mm; Optional by agreement at enquiry and order
EN 10283 · Edition 2019
[2] Impact Energy: KV2 as specified in
ISO 11972 · Edition 2023
[3] Impact Energy: Verification of impact tests is required only when indicated by the customer.
Welding Conditions
EN 10213–2007+A1:2016
EN 10283–2019
EN 10340–2007
Notes
EN 10213 · Edition 2007+A1:2016
[1] Preheat: Production welding by the foundry; requirements for austenitic/austenitic-ferritic grades are normative.; Preheat temperature depends on casting geometry, thickness and climatic conditions.
[2] Interpass Temperature: Production welding by the foundry; requirements for austenitic/austenitic-ferritic grades are normative.
[3] Post-weld Heat Treatment: Production welding by the foundry; requirements for austenitic/austenitic-ferritic grades are normative.; In general, production welds are major when prepared cavity depth exceeds 40% of the wall thickness; minor weld corrosion conditions may require special agreement.
EN 10283 · Edition 2019
[4] Preheat: Preheat depends on casting geometry, thickness and climatic conditions.
[5] Post-weld Heat Treatment: minor welds; Special arrangements may be agreed according to corrosion conditions. With low preheat and interpass temperatures (≤150 °C), post-weld heat treatment may be suppressed by agreement.
[6] Post-weld Heat Treatment: major welds; Special arrangements may be agreed according to corrosion conditions. With low preheat and interpass temperatures (≤150 °C), post-weld heat treatment may be suppressed by agreement.
EN 10340 · Edition 2007
[7] Preheat: Preheat depends on casting geometry, thickness and climatic conditions.
[8] Post-weld Heat Treatment: For minor welds, special arrangements may be agreed according to corrosion conditions; production welds are generally major when cavity depth exceeds 40% of wall thickness. Special arrangements may be agreed according to corrosion conditions.
Applications
Typical casting applications include architectural cast components where corrosion resistance and surface finish are required. Other cast components used in this material family include pump casings, impellers, valve bodies, covers and pipe fittings. Typical settings include chemical and pharmaceutical plants, food and beverage machinery, and filling, mixing and liquid-handling systems.
Need GX2CrNiMo19-11-2 Castings?
Contact us for casting and machining inquiries.
Email Us for a QuoteLast Updated: November 6, 2026