GX12CrMoVNbN9-1 (EN 1.4955) High-Alloy Steel Casting Material
High-Alloy Steel
Introduction
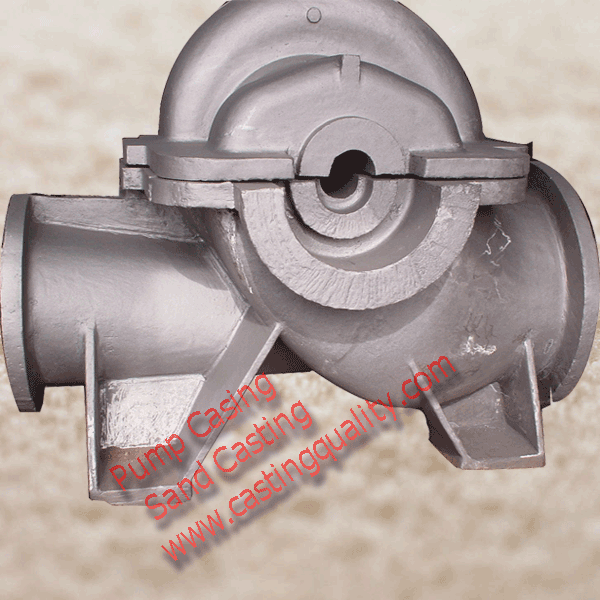
GX12CrMoVNbN9-1 is a high-alloy steel casting grade covered by EN 10213. Typical family applications include valve bodies, pump casings and fittings.
| Field | Value |
|---|---|
| Designation | GX12CrMoVNbN9-1 (EN 1.4955) |
| Material Type | Alloy Steel |
| Sub Type | High-Alloy Steel |
| Product Form | casting |
Manufacturing Process
Investment Casting
Shell Molding Casting
Sand Casting
Equivalent Materials
N/A
Similar Materials
N/A
Reference Standards
| Standard | Standard Title | Edition | Specification | Identifier |
|---|---|---|---|---|
| EN 10213 | Steel castings for pressure purposes | 2007+A1:2016 | GX12CrMoVNbN9-1 | — |
Related Casting Products


Physical Properties
| Property | Value / Unit | Note | Source |
|---|---|---|---|
| Density | 7.77 kg/dm³ | Test at 20 °C | EN 10213 |
| Thermal Expansion | 10.8 ×10⁻⁶/K | Temperature range: 20–100 °C | EN 10213 |
| Thermal Expansion | 11.5 ×10⁻⁶/K | Temperature range: 20–300 °C | EN 10213 |
| Thermal Expansion | 12.1 ×10⁻⁶/K | Temperature range: 20–500 °C | EN 10213 |
| Thermal Conductivity | 25.7 W/(m·K) | Test at 50 °C | EN 10213 |
| Thermal Conductivity | 26.4 W/(m·K) | Test at 100 °C | EN 10213 |
| Specific Heat | 456 J/(kg·K) | Test at 20 °C | EN 10213 |
| Magnetic Property | Magnetic | EN 10213 |
Chemical Composition
| Element | EN 10213Edition 2007+A1:2016 · wt.%Cast analysis |
|---|---|
| C | 0.10–0.14 |
| Si | 0.20–0.50 |
| Mn | 0.30–0.80 |
| P | ≤ 0.020 |
| S | ≤ 0.010 |
| Cr | 8.00–9.50 |
| Ni | ≤ 0.40 |
| Mo | 0.85–1.05 |
| N | 0.030–0.070 |
| Nb | 0.06–0.10 |
| V | 0.18–0.25 |
| Al | ≤ 0.020 |
Heat Treatment
EN 10213–2007+A1:2016 · QT
Notes
EN 10213 · Edition 2007+A1:2016
[1] QT: Treatment temperatures are given for information; required delivery condition is specified separately.
Mechanical Properties
Core Mechanical Properties
Additional Mechanical Properties
Notes
EN 10213 · Edition 2007+A1:2016
[1] Yield Strength (Rp0.2)/Tensile Strength/Elongation/Impact Energy: wall thickness ≤ 200 mm; Properties verified on test blocks of thickness up to 150 mm; applicability to casting wall thickness as stated. Larger governing thickness requires agreement.; Room temperature
[2] Yield Strength (Rp0.2): Test at 100 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[3] Yield Strength (Rp0.2): Test at 200 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[4] Yield Strength (Rp0.2): Test at 300 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[5] Yield Strength (Rp0.2): Test at 350 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[6] Yield Strength (Rp0.2): Test at 400 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[7] Yield Strength (Rp0.2): Test at 450 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[8] Yield Strength (Rp0.2): Test at 500 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[9] Yield Strength (Rp0.2): Test at 550 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[10] Yield Strength (Rp0.2): Test at 600 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
[11] Yield Strength (Rp0.2): Test at 625 °C; Verification of elevated-temperature yield values is subject to agreement at enquiry and order.
Welding Conditions
EN 10213–2007+A1:2016
Notes
EN 10213 · Edition 2007+A1:2016
[1] Preheat: Production welding by the foundry; ferritic/martensitic guidance is informative.; Preheat temperature depends on casting geometry, thickness and climatic conditions.
[2] Interpass Temperature: Production welding by the foundry; ferritic/martensitic guidance is informative.
[3] Post-weld Heat Treatment: Production welding by the foundry; ferritic/martensitic guidance is informative.; In general, production welds are major when prepared cavity depth exceeds 40% of the wall thickness; minor weld corrosion conditions may require special agreement.
Applications
For high-alloy steel EN 10213 GX12CrMoVNbN9-1, typical cast components in this material family include valve bodies, pump casings and fittings. Applications include industrial process plants, heating circuits and power-generation equipment. Service medium, temperature, material condition and the finished equipment design determine the permitted duty; the grade name alone is not an operating rating.
Need GX12CrMoVNbN9-1 Castings?
Contact us for casting and machining inquiries.
Email Us for a QuoteLast Updated: November 6, 2026